Fonterra Clandeboye Mozzarella Plant, New Zealand
Aurecon and partners take a collaborative approach to Fonterra's Clandeboye plant, using 3D modelling to modularise their cheese-making process.


Change your location to view content tailored for you.
Aurecon supported Fonterra to realise an innovative water recycling project at their Maungatūroto dairy factory, reducing water usage at the site by up to 25 per cent.
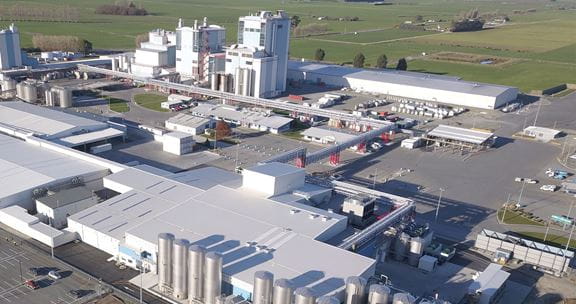
The factory processes milk to create milk powder and various dairy end products. An evaporation process is used to extract the components to create milk powder, with evaporator condensate (water extracted from milk) as an effluent. With increasing droughts in the area over the past few summers, Fonterra had been exploring options to recover and reuse this evaporator condensate.
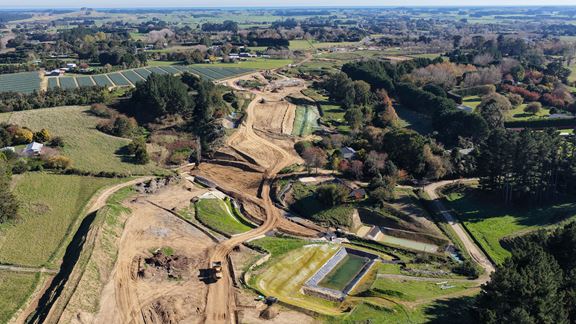
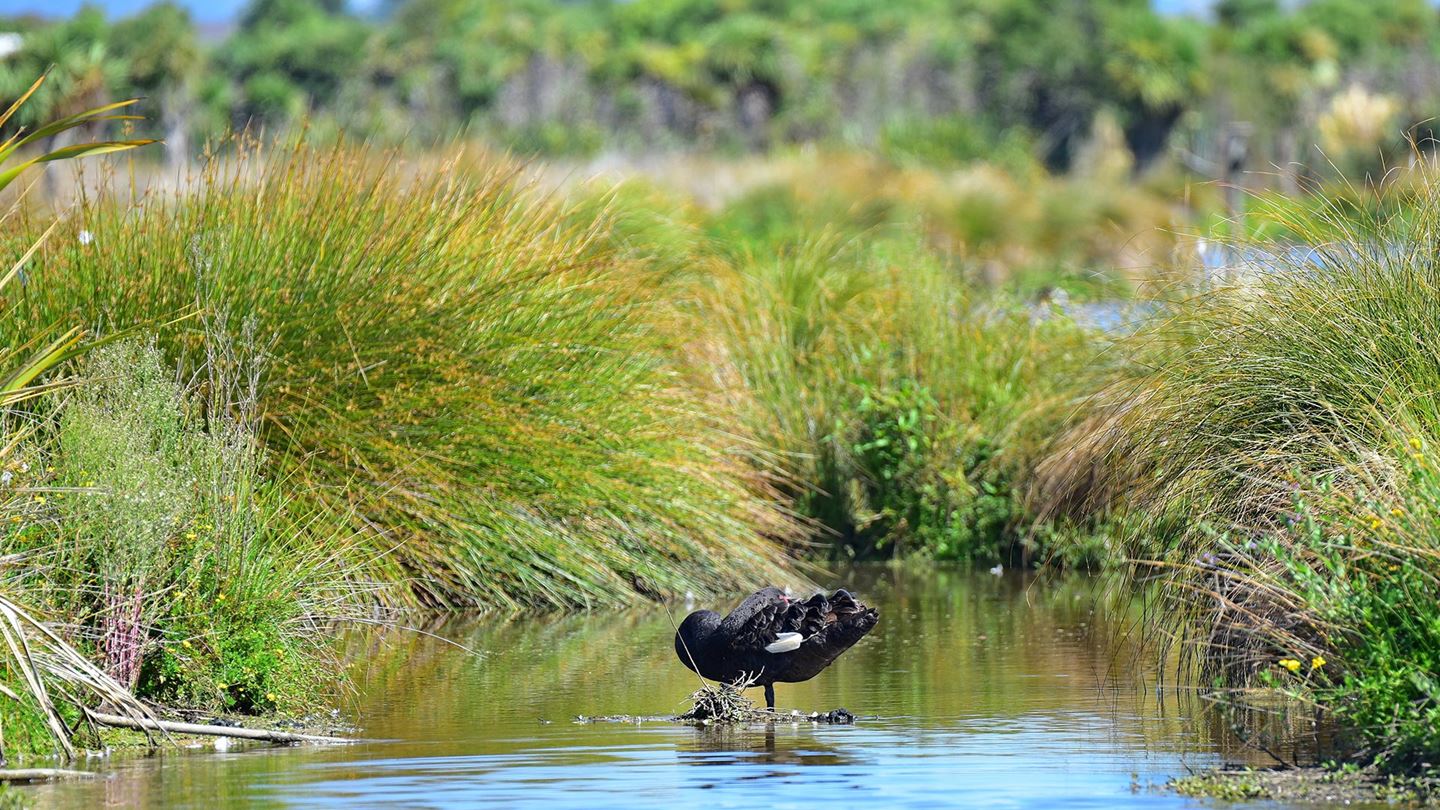
The factory developed an idea to leverage an existing wetland on the site that acts as a natural bioreactor to filter the evaporator condensate before it is discharged to the adjacent Wairau River. The biota within the wetland removes nutrients and organics in the evaporator condensate before it is discharged into the river under Fonterra Maungaturoto’s resource consent conditions.
This project considered collection of the wetland treated evaporator condensate, before directing it through the site's water treatment plant for reuse in the processing plant and for drinking water – taking what is essentially a waste product, and with extra processing, creating a useful process input.


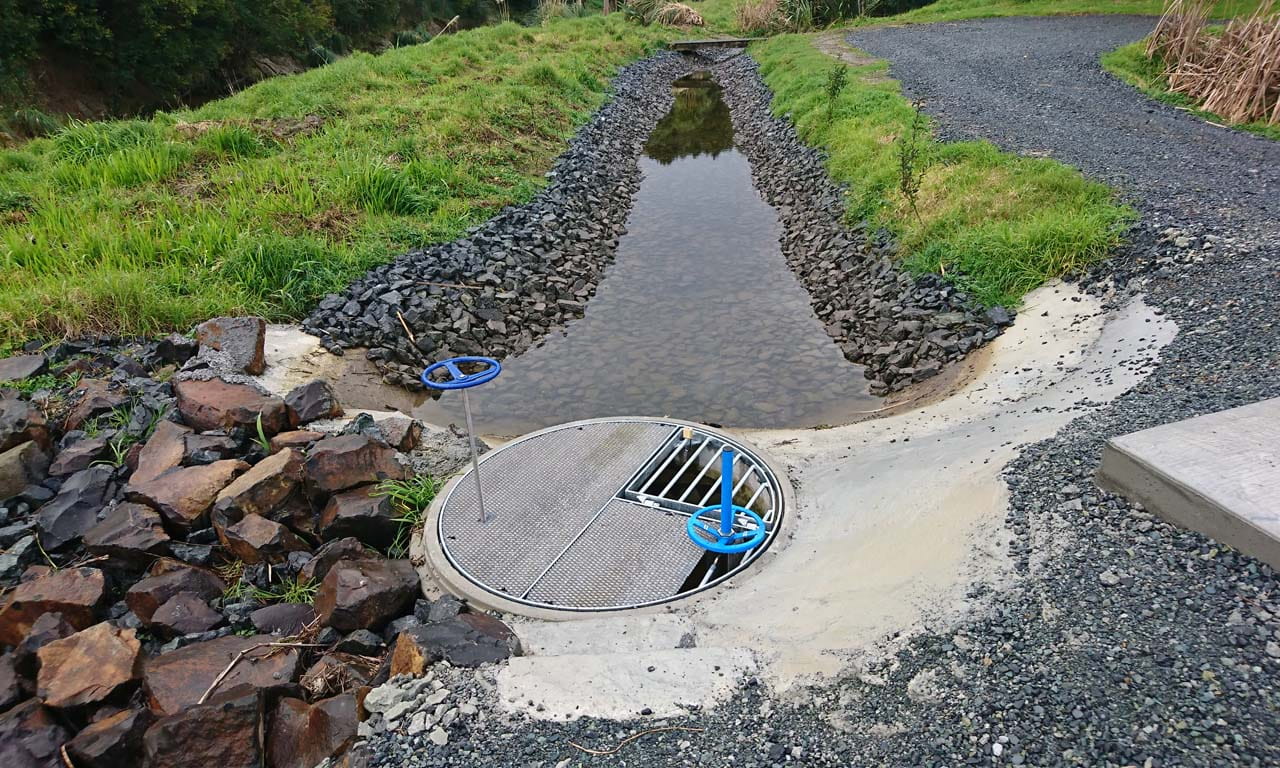
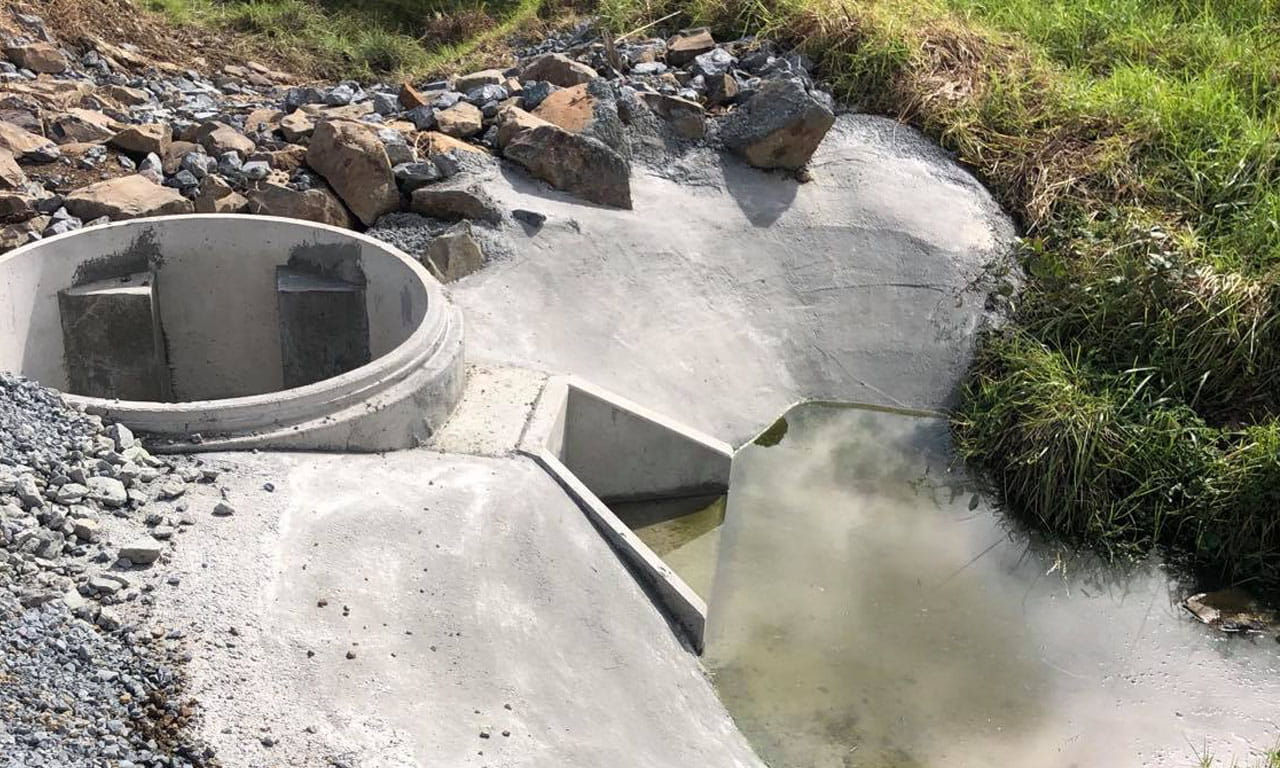
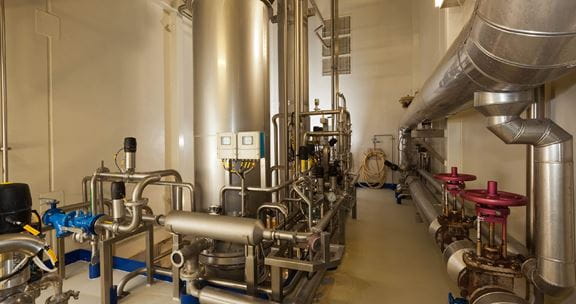
Fonterra initially engaged Aurecon to undertake a feasibility study to secure capital funding. With the viability of the scheme proven, our team was engaged to deliver the design, construction monitoring and commissioning, and facilitate the hazard and operability workshop. Our team designed a collection wingwall and sump within the wetland stream, pump chamber, rising main, sampling system and integrated a new UV reactor in the existing treatment plant.
Completed in 2021, the wetland recycling process is now producing between 500,000 to 700,000 litres of water per day – representing about a quarter of the water being used throughout the site’s processing plants. Fonterra believes the model could be implemented at other manufacturing sites in New Zealand and worldwide.
Realising the ambitious project required working through challenges such as maintaining the ecosystem within the wetland, preventing any risk to food safety quality, and not interrupting the site’s efficiency to operate.
Biodiversity is maintained with rigorous testing. The evaporator condensate is tested for turbidity, conductivity, pH and temperature before it enters the wetland environment, and again before it is brought back into the processing plant. The 10,000 sq m wetland is well established with flaxes, reeds and trees, and Fonterra has supported this with additional planting to further enhance biodiversity.
The testing methodology adopted for the wetland underpins food safety. It has been further enhanced by the introduction of a UV reactor which provides an extra level of sterilisation for the entire site. This achieves the required water purity level of Log 3 (99.9 per cent reduction of micro-organisms).
The early involvement of technical experts during the feasibility stage enabled a faster delivery of the design and construction of the new systems to ensure Fonterra’s manufacturing schedules weren’t disrupted.
Fonterra’s water reclaiming initiative is delivering tangible outcomes, reducing their reliance on the Kaipara District Council supply, in turn reducing capital costs and providing greater resilience for the surrounding community. Local Iwi Te Uri o Hau and the Northland Regional Council have viewed the project positively.
The water-saving initiative has received recognition for its innovation, as a finalist in the 2021 Sustainable Business Network Awards and winner of the inaugural Environmental Sustainability Project Award at the 2021 Water NZ Awards.
Following the success of this project, the Maungatūroto factory is now exploring further water-conservation measures to try to achieve savings of up to 50 per cent.
This project has won the following awards:
Aurecon and partners take a collaborative approach to Fonterra's Clandeboye plant, using 3D modelling to modularise their cheese-making process.
Aurecon designs and installs of an innovative evaporator and lactose concentrate load-in facilities at the Fonterra Hautapu Dairy Factory site.
Aurecon is part of the Northern Alliance delivering NZ’s Ō2NL expressway, partnering with NZTA Waka Kotahi to improve safety, reliability and efficiency.