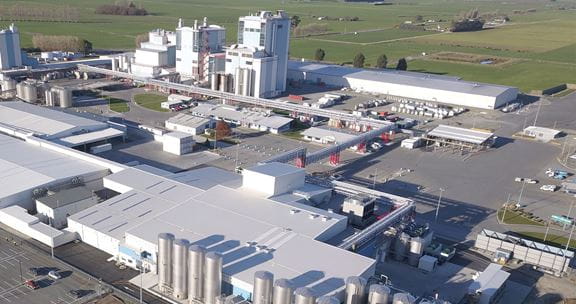
Fonterra Clandeboye Mozzarella Plant, New Zealand
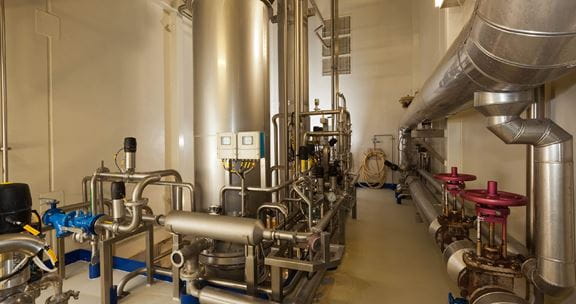
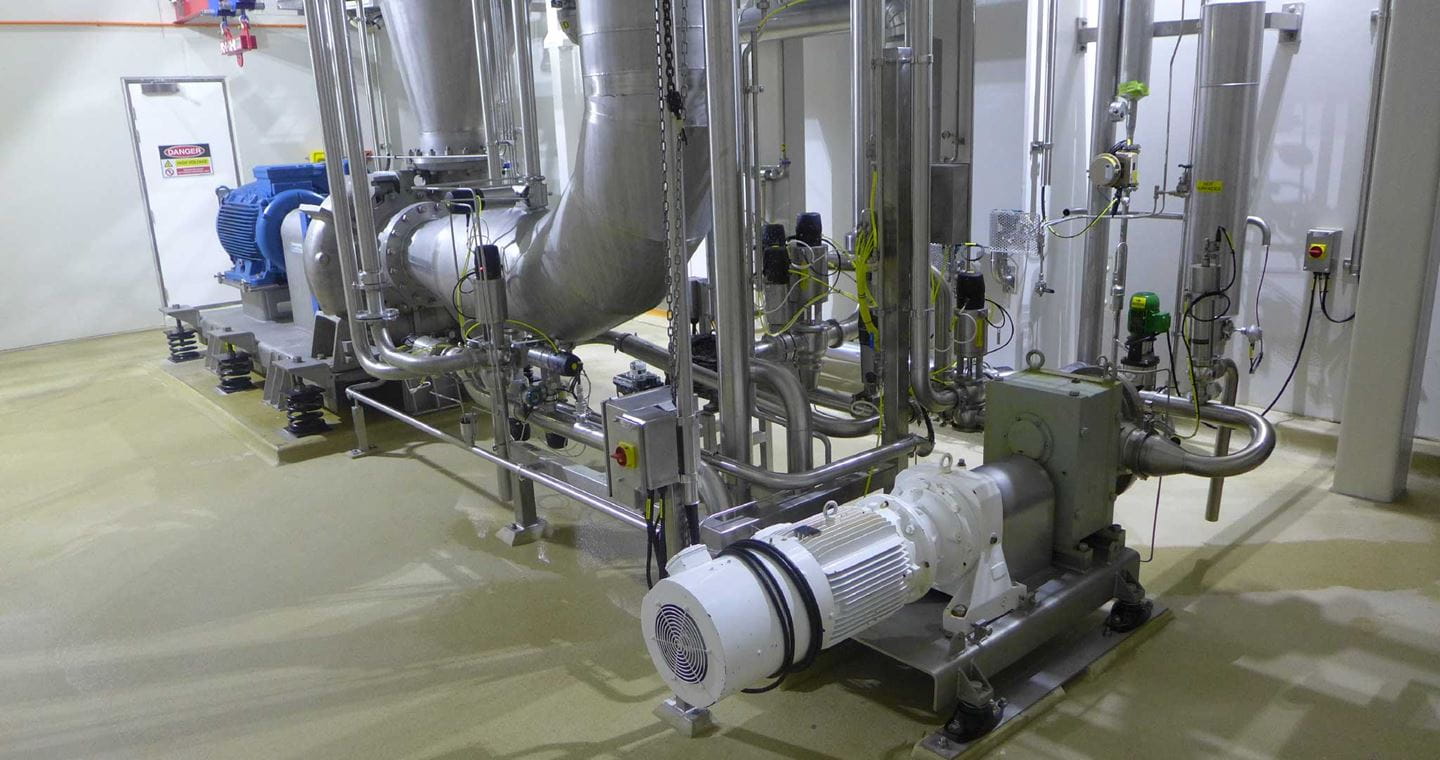
Aurecon and partners take a collaborative approach to Fonterra's Clandeboye plant, using 3D modelling to modularise their cheese-making process.


Change your location to view content tailored for you.
In 2013 Fonterra Co-operative Group (Fonterra), the largest manufacturer of dairy products in New Zealand, required an increased yield of edible grade lactose from their existing lactose plant on the Clandeboye dairy factory site.
The most substantial challenge, given the novelty of the technology, was to achieve the target process performance, an increased plant product yield from a nominal 64 per cent to 76 per cent, without the use of any additional raw material.
Aurecon was engaged to design, engineer and project manage the installation of a new lactose crystallising evaporator.
We also delivered all project management, process, mechanical, structural, electrical and automation design work for the new evaporator; prepared contracts for the installation works; and commissioned the completed plant.
The evaporation plant used in the lactose manufacturing process typically operates at high solids concentrations. These process conditions often result in significant fouling of evaporator heat transfer surfaces which necessitates regular cleaning and results in lost production time and the formation of small crystals in the downstream batch cooling crystallisation process.


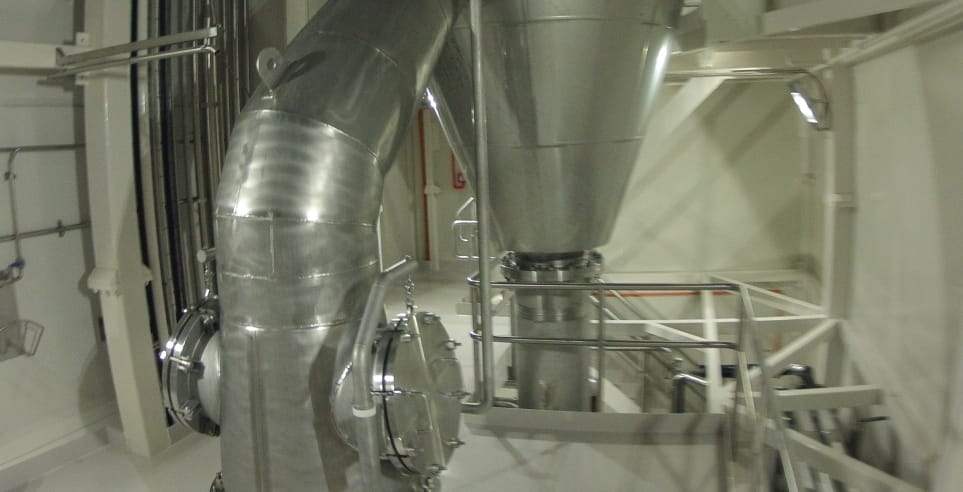
Aurecon’s innovative design, which also incorporated features to improve lactose crystal growth, dramatically reduced heat transfer surface fouling. The novel design provides extended product run times, improved product yield, reduced water and chemical requirements for cleaning, lower product losses, and less wastewater generation than existing evaporator options.
The project increased the plant’s lactose manufacturing capacity by more than 25 per cent without using any additional raw material and enabled the recovery of lactose for incorporation in higher value export dairy products that previously Fonterra would have sold as a low value animal feed or spray irrigated on land.
The success of this project has established a new engineering standard and best practice for the production of lactose.
At the same plant, Aurecon designed New Zealand’s first modular construction at scale for the upgraded mozzarella processing plant.
The project has won the following award:
Aurecon and partners take a collaborative approach to Fonterra's Clandeboye plant, using 3D modelling to modularise their cheese-making process.
Aurecon designs and installs of an innovative evaporator and lactose concentrate load-in facilities at the Fonterra Hautapu Dairy Factory site.
Aurecon is delivering human-centred modular design to three new rail stations with integrated transport options for Auckland's southern growth area.